
Recommended High-Performance Laser Systems
Verified hardware solutions for heavy-duty metal marking, precision UV micro-machining, automated pipe cutting, and high-speed industrial traceability.
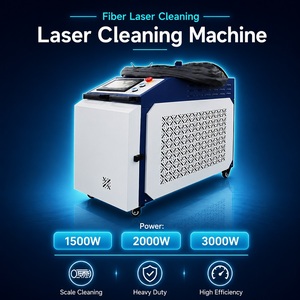
Bluetimes Mobile 1500W 2000W 3000W Continuous Wave Fiber Laser Cleaning Machine Easy to Operate
- High Efficiency Oxide & Rust Stripping
- Ergonomic Handheld Optics Head
- 1500W - 3000W Fiber Source
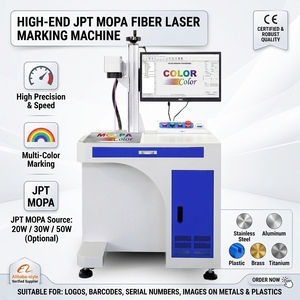
New Industrial 50W Fiber Laser Marking for Metal JPT MOPA Source Color Marking Machine PLT/BMP for Stainless Steel 2026 CE
- Tunable Pulse Duration (2-500ns)
- Stainless Steel Vivid Color Annealing
- CE Certified Industrial Enclosure
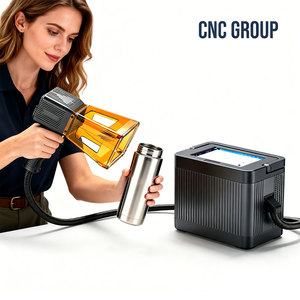
New Portable Metal 20W CNC 3D Desktop Mini Fiber Laser Marking Machine with DXF/AI/DST Support Price
- 3D Dynamic Curved Surface Focus
- Multi-Format Vector Support (AI/DXF)
- Compact Desktop Workstation
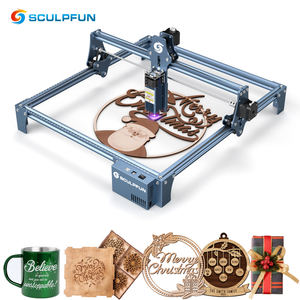
SCULPFUN S9 90W Laser Engraver 3d CNC Desktop Printer Laser Engraving Machines
- Ultra-Fine 0.06mm Laser Spot
- Full Metal Structure Fast Assembly
- Wood, Acrylic & Metal Marking
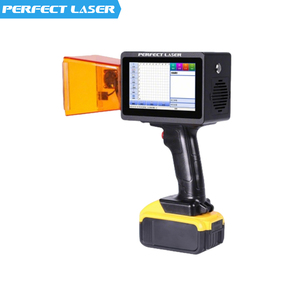
Perfect Laser Handheld Portable Metal Acrylic Gold Silver Rubber Wood Marker Mini Fiber Laser Marking Machine with LCD Screen
- Touchscreen LCD Control Interface
- Ultra-Portable On-Site Marking
- Multi-Material Substrate Versatility
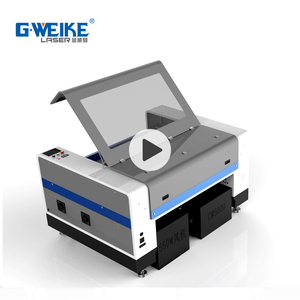
G.WEIKE 150 Watts 400 Watt Acrylic CO2 Laser Cutting Machine
- 150W - 400W High Peak CO2 Tube
- Thick Acrylic & Wood Precision Cutting
- Heavy Industrial Chassis Stability
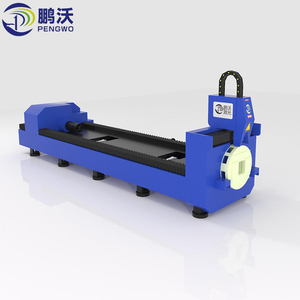
3000W Automatic Feeding CNC Industrial Laser Pipe Cutting Machine Metal Tube Fiber Laser Cutter AI Graphic Direct Manufacturer
- Automated Bundle Pipe Feeding System
- AI-Driven Nesting & Graphic Import
- 3000W Heavy Duty Fiber Engine
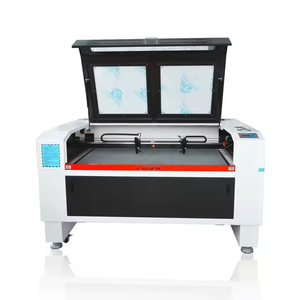
Fully automatic 6090/1390/1610 CO2 laser cutting machine for acrylic board
- Multiple Bed Sizes (6090, 1390, 1610)
- Automated Pass-Through Architecture
- Smooth Edge Polished Acrylic Finish
Engineering Authority & E-E-A-T Quality Standards
When procuring industrial laser marking, engraving, and cutting machinery, evaluating raw laser source output is insufficient. Tier-1 manufacturers differentiate through beam optical delivery, dynamic 3-axis galvanometer focus compensation, long-term thermomechanical stability, and rigorous compliance with international safety protocols (CE compliance and ISO 9001 quality management systems).
Comprehensive Procurement Analysis: Evaluating 3D Laser Marking Infrastructure
Modern advanced manufacturing—spanning aerospace components, medical device UDI serialization, automotive electronics, and precision consumer goods—demands indelible, high-contrast, non-destructive part identification. Legacy 2D planar marking systems, constrained by fixed focal distances and flat field F-theta lenses, fail when processing stepped geometries, complex cylindrical curves, inclined planes, or deep cavities.
1. Technical Wavelength Matrix: Selecting the Optimum Laser Architecture
Choosing the incorrect laser wavelength is the single largest cause of capital misallocation in industrial laser procurement. Below is an engineering evaluation of the primary active laser mediums utilized by leading global exporters:
- MOPA Fiber Lasers (1064nm Wavelength): Master Oscillator Power Amplifier (MOPA) architecture provides independent control of pulse frequency (1kHz to 4000kHz) and pulse duration (2ns to 500ns). This enables damage-free black annealing on medical-grade 316L stainless steel, high-contrast white marking on anodized aluminum, and carbonization-free marking on engineered polymers (ABS, Nylon, PBT).
- Cold UV Lasers (355nm Wavelength): Operating via third-harmonic generation (THG), UV lasers utilize ultra-short ultraviolet photons to break molecular bonds directly (photodecomposition) rather than vaporizing material thermally (pyro-decomposition). UV systems produce zero heat-affected zones (HAZ), making them essential for delicate glass etching, medical catheter marking, and heat-sensitive HDPE/PVC packaging.
- CO2 Laser Generators (10.6μm / 9.3μm Wavelength): Ideal for non-metallic organic substrates. High-power CO2 laser systems cut and engrave dense acrylics, timber, textiles, leather, and architectural laminates with flame-polished edge quality and high speed.
2. Comparing Dynamic 3D Marking vs. Legacy 2D + Rotary Indexing
To assist global procurement officers, plant engineering directors, and OEM buyers in selecting the appropriate laser platform, the technical matrix below highlights key operational parameters:
| Performance Feature | Legacy 2D Galvo + Rotary Axis | Advanced 3D Dynamic Focus System | Procurement ROI Impact |
|---|---|---|---|
| Surface Processing | Strictly Flat Surfaces or Simple Cylinders | Complex 3D Curves, Spheres, Slopes, Steps | Expands job capabilities by 300% |
| Focus Adjustment | Manual/Motorized Mechanical Z-Tower | Microsecond Optical Dynamic Lens Focal Shift | Eliminates tool set-up downtime between batches |
| Marking Field Depth | Limited to Lens Focal Depth (±1mm to ±3mm) | Wide Dynamic Range (Up to ±80mm to ±120mm) | Allows single-pass marking on deep components |
| Distortion & Edge Blur | Beam spot elongates at field edges | Real-time software aberration & focal correction | Ensures 100% 2D DataMatrix code readability |
| Automation Integration | Requires complex multi-axis indexing robotics | Direct vision system + 3D laser head scanning | Reduces line integration costs by up to 45% |
Proven Manufacturing Solutions Across Regulated Sectors
Aerospace Part Traceability
Permanent MIL-STD-130 compliant direct part marking (DPM) on titanium, inconel, and aircraft-grade aluminum. Deep metal engraving withstands thermal barrier coatings, abrasive environments, and lifecycle stress testing.
Medical Device UDI Serialization
Corrosion-free black annealing on stainless surgical instruments and cold UV laser marking on implantable polymers compliant with FDA UDI regulations and ISO 13485 standards. Withstands repeated autoclave cycles.
Automotive DMC & VIN Marking
High-speed inline laser coding of Data Matrix codes onto engine blocks, transmission gears, and electrical connectors. Seamless integration with factory MES/ERP networks for 24/7 automated batch tracking.
Strategic Forecast: 3D Laser Marking Procurement Trends (2026–2030)
As global manufacturing transitions toward Industry 4.0 and autonomous smart factories, the requirements for laser marking machinery are evolving rapidly. Procurement managers and system integrators must anticipate four core macro trends over the coming decade:
Trend 1: AI Vision Alignment & Dynamic Autofocus Offset
Traditional mechanical fixtures and physical jigs are being replaced by high-resolution CCD camera vision systems integrated co-axially within the optical beam path. Combined with AI-driven pattern recognition software, modern 3D laser markers automatically identify part orientation, height deviations, and spatial tilt, dynamically recalculating laser paths in under 15 milliseconds without manual operator alignment.
Trend 2: Seamless Cobot & Robotic Cell Integration
Unattended 24/7 production demands plug-and-play compatibility between laser workstations and Collaborative Robots (COBOTs). Leading exporters now offer standardized I/O protocols (Profinet, EtherNet/IP, OPC UA) that allow COBOT arms to perform automated loading, 3D laser marking, optical code verification, and sorting without human intervention.
Trend 3: Ultra-Short Pulse (Picosecond & Femtosecond) Market Penetration
While nanosecond MOPA fiber lasers remain the workhorse for standard industrial marking, ultrashort pulse lasers (USP) are rapidly dropping in price. Delivering pulse widths in the picosecond and femtosecond range, these laser sources enable cold micromachining with virtually zero thermal diffusion, creating hydrophobic micro-textures, non-glare black surfaces on anodized aluminum, and sub-micron semiconductor wafer scribing.
Trend 4: Sustainable Green Energy Fiber Laser Architecture
With global sustainability mandates and rising industrial electricity costs, thermal management efficiency is a critical evaluation benchmark. Next-generation fiber laser power sources achieve wall-plug electrical efficiency exceeding 35%, drastically reducing ambient heat generation, cooling requirements, and overall carbon footprint during continuous operation.
Why Global Manufacturers Choose Our Technology Platforms
10-Year Warranty & Reliability
Engineered with military-spec structural aluminum frames and premium optical galvos. Backed by industry-leading warranty coverage and technical SLAs across 46 countries worldwide.
3D Dynamic Focus Standard
Eliminate complex setup procedures. Our 3-axis galvo beam expander maintains diffraction-limited laser spot sizes across slanted, curved, and irregular 3D workpiece geometries.
CE & ISO 9001 Compliance
Built strictly under accredited quality management frameworks. Interlocked Class 1 safety enclosures protect operators from stray radiation, meeting global regulatory compliance.
Frequently Asked Questions for Procurement Decisions
How does a 3D laser marker maintain precise focal spot size across curved surfaces?
A true 3D laser marking system incorporates an active optical z-axis focal shifting lens positioned before the two-axis galvo scanning mirrors. Guided by 3D CAD vectors (such as STL, STEP, or IGES format), the high-speed linear motor dynamically alters the expanding lens position in real time. This compensates for distance fluctuations down to microsecond intervals, maintaining a constant spot diameter and focal plane across slopes, steps, cones, and spheres.
What is the primary difference between MOPA fiber lasers and standard Q-switched fiber lasers?
While Q-switched fiber lasers operate at fixed pulse durations (typically 100ns to 120ns), MOPA (Master Oscillator Power Amplifier) fiber lasers allow independent tuning of both pulse duration (2ns to 500ns) and repetition rate (1kHz to 4MHz). Short pulse widths minimize thermal diffusion, enabling damage-free dark annealing on stainless steel and high-contrast marking on delicate plastics, whereas longer pulses excel at deep metal engraving.
Can we request free sample testing on our specialized materials before placing a purchase order?
Yes. We strongly encourage global procurement teams to submit sample materials to our UK application laboratory. Our optics specialists perform comprehensive wavelength testing, pulse optimization, contrast validation, and code readability checks (ISO 15415 / 15416 standards), delivering a complete technical report and video evaluation prior to machinery commitment.
What international safety standards and laser class certifications do your machines adhere to?
All supplied laser systems comply fully with EN 60825-1 laser safety protocols and CE regulations. Enclosed production systems feature Class 1 dual-channel safety interlocks, certified protective optical viewing windows, integrated fume extraction ports, and emergency shutoff hardware ensuring complete operator safety during continuous factory operation.
How are international service, installation, and technical support handled for overseas facilities?
We maintain an authorized global service network across 46 countries. International clients receive rapid remote diagnostic support, software calibration guidance, and fast-tracked spare parts dispatch. Field service engineers are available for onsite installation, integration training, and routine preventative maintenance audits.