
Precision Industrial Systems
Aerospace-Grade Laser Marking & Processing Machinery
Engineered for high-reliability material identification, clean surface preparation, and seamless component traceability across Swedish aerospace & high-tech manufacturing ecosystems.
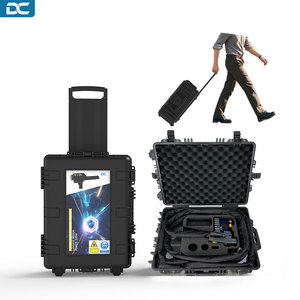
Dachuan Handheld 500W Portable Pulsed Fiber Laser Cleaner Wood Metal Stone Stainless Steel Aluminum Paper Laser Cleaning Machine
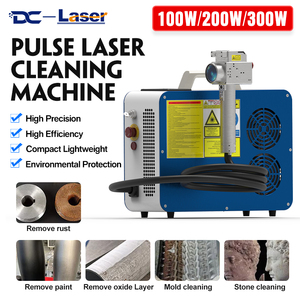
Portable Handle Pulse JPT Laser Rust Removal Cleaner 50w 100w 200w 300w Laser Cleaning Machine for Wood Metal
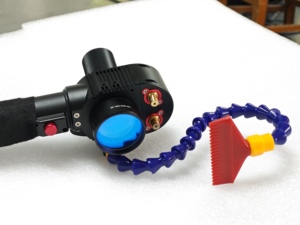
800g Lightweight 300W Handheld MOPA Pulse Laser Cleaning Gun DHCP30 Pro with Built-in Blowing Air and QCS Connector
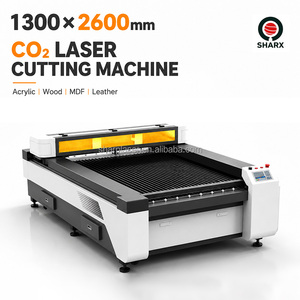
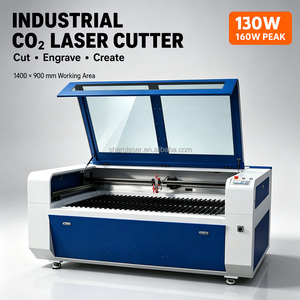
150W 1325 CO2 Laser Cutter with Ruida Control System Water-Cooled for Wood Acrylic MDF Stone Rubber Supporting DXF/PLT Formats
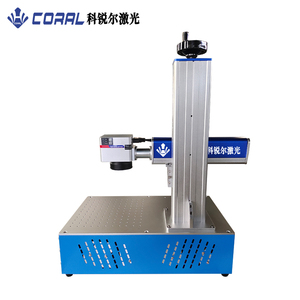
Wholesale Price HG-ZM-A-D20 Engraving Engraver Machine Laser Marking Machine Fiber Laser Marking Machine With Hot Sale
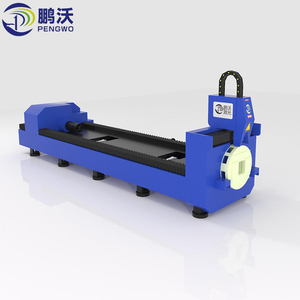
3000W Automatic Feeding CNC Industrial Laser Pipe Cutting Machine Metal Tube Fiber Laser Cutter AI Graphic Direct Manufacturer
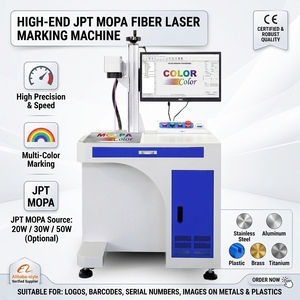
New Industrial 50W Fiber Laser Marking for Metal JPT MOPA Source Color Marking Machine PLT/BMP for Stainless Steel 2026 CE
Engineering Whitepaper
Direct Part Marking (DPM) & Structural Integrity in Swedish Aerospace Manufacturing
An in-depth analysis of laser beam dynamics, thermal zone mitigation, and data matrix machine readability across critical flight hardware substrates.
In the modern global aerospace ecosystem, non-negotiable component traceability is governed by strict international frameworks including AS9100 Rev D, EN 9100, MIL-STD-130, NASA-STD-6002, and ATA Spec 200. As Sweden expands its advanced aerospace production hubs—ranging from military airframe manufacturing in Linköping to aero-engine component fabrication in Trollhättan and orbital launch technologies at Spaceport Esrange—the demand for ultra-precise, zero-defect Direct Part Marking (DPM) systems has reached an all-time peak.
1. Thermal Metallurgical Impact & Zero Heat-Affected Zone (HAZ) Annealing
Aerospace components manufactured from high-performance alloys—such as Titanium 6Al-4V, Inconel 718, 300-series Stainless Steels, and 7075-T6 Anodized Aluminum—are subjected to extreme mechanical fatigue, thermal stress cycles, and corrosive environments. Traditional mechanical engraving, dot peen, or high-power thermal etching can induce localized micro-fractures, stress concentrations, or alter the crystalline grain structure of the alloy.
To overcome structural degradation, our advanced MOPA (Master Oscillator Power Amplifier) Fiber Laser Systems utilize adjustable pulse durations ranging from 2 ns to 500 ns. By tuning pulse frequencies up to 4000 kHz, operators can execute ultra-clean oxide surface annealing without penetrating or melting the underlying base substrate. This creates high-contrast, permanent dark marks via controlled surface oxidation while maintaining absolute fatigue resistance and micro-structural density.
2. 2D Data Matrix Reliability & ISO/IEC 15415 Grade Requirements
Aerospace part identification requires long-term readability through component assembly, aggressive chemical cleaning (skydrol hydraulic fluid, de-icing agents), thermal treatments, and decades of operational maintenance. Laser-marked Data Matrix ECC 200 codes must achieve ISO/IEC 15415 and ISO/IEC 16022 grade 'A' or 'B' verification standards.
Our 3-Axis Dynamic Focusing Galvo technology maintains sub-micron focal alignment across 3D contoured, tilted, or cylindrical surfaces without requiring mechanical Z-axis re-positioning. This ensures consistent symbol contrast, cell axial non-uniformity control, and perfect grid alignment across complex geometry engine blades, structural spars, and fuel manifolds.
| Laser Wavelength & Source | Primary Aerospace Substrates | Marking Mechanism | HAZ / Thermal Impact | Applicable Standards |
|---|---|---|---|---|
| MOPA Fiber (1064 nm) | Titanium 6Al-4V, Inconel, Stainless Steel, Aluminum 7075 | Controlled Oxide Annealing / Sub-surface contrast | Negligible (Sub-micron level) | MIL-STD-130, AS9100, ATA Spec 200 |
| UV Cold Laser (355 nm) | Heat-sensitive Plastics (PEEK, PTFE), Glass, Composites | Photochemical "Cold" Photodecomposition | Zero Thermal Impact | NASA-STD-6002, ISO/IEC 16022 |
| CO2 Galvo (10600 nm) | Carbon Fiber Composites, Non-metallic Seals, Packaging | Thermal Surface Deposition & Ablation | Low to Medium (Substrate dependent) | EN ISO 11553, CE Compliance |
Swedish Aerospace Ecosystem
Localized Application Scenarios across Sweden's High-Tech Hubs
Tailored laser identification systems designed to integrate directly into Swedish industrial workflows, defense sub-contracting facilities, and aerospace research centers.
Linköping Defense & Airframe Manufacturing
Direct Part Marking on lightweight carbon-fiber composite panels and high-strength aluminum spars for military airframe programs. High-contrast 2D Data Matrix codes withstand extreme aerodynamic drag and environmental degradation.
Trollhättan Aero-Engine Propulsion Systems
Black oxide annealing on single-crystal superalloy turbine blades and Inconel combustor components. Zero-defect laser pulse control prevents micro-fracturing under intense thermomechanical fatigue.
Spaceport Esrange (Kiruna) Satellite & Payload ID
Cold UV laser marking on delicate spacecraft electronics, solar cell connectors, and heat-shield insulation packages. Prevents outgassing and ensures zero thermal damage to ultra-sensitive satellite hardware.
Industry 4.0 & Sustainability
Emerging Trends Driving Swedish Aerospace Purchasing Decisons
How Swedish industrial engineering standards are shaping the next generation of laser part identification technology.
Fossil-Free Steel & Green Supply Chain Integration
Sweden is leading the global green transition with fossil-free steel initiatives (such as SSAB's HYBRIT technology). Swedish aerospace suppliers demand laser marking machinery built with energy-efficient fiber sources, low power standby draw, and recyclable mil-spec structural aluminum enclosures to comply with strict national ESG targets.
Cobot-Assisted Automated Batch Marking Cells
To optimize high-cost Swedish technical labor, factories are implementing fully automated laser cells integrated with Collaborative Robots (Cobots), automatic data plate loaders, and inline vision system inspection. Machines must support Profinet, EtherCAT, and TCP/IP protocols for zero-touch digital twin manufacturing line integration.
Engineering Excellence
Why Leading European Aerospace Manufacturers Choose Our Systems
Built under ISO 9001 certified management, delivered with CE compliance, and backed by robust European technical support networks.
ISO 9001 & CE Certification
Fully compliant with European Laser Safety Directives (EN 60825-1 Class 1 enclosures). Every machine undergoes rigorous optical beam stability testing prior to shipment.
Integrated 3D Dynamic Focusing
Standard 3-axis software control keeps laser spot size and energy density constant across complex, curved aerospace geometries up to ±40 mm depth of focus.
Dedicated European After-Sales Network
Supported across 46 countries with rapid spare parts logistics, remote optics diagnostics, and on-site training for Swedish technical personnel.
Procurement & Technical Support
Frequently Asked Questions by Swedish Aerospace Buyers
Addressing compliance, local machine delivery, material sample testing, and technical support standards in Sweden.
Which laser technology is best suited for marking aerospace titanium parts in Sweden?
MOPA Fiber Laser systems are the industry standard for aerospace titanium (such as Ti-6Al-4V). By adjusting pulse duration (down to 2-4 ns), engineers can produce deep black annealed 2D Data Matrix codes without thermal micro-cracking or changing the underlying structural properties of the metal.
Are your machines compliant with Swedish Work Environment Authority (Arbetsmiljöverket) safety requirements?
Yes. All systems delivered to Sweden are fully CE compliant and classified as Class 1 laser systems with integrated safety interlocks, optical viewing windows, and industrial fume extraction connections meeting EN 60825-1 safety standards.
Can we request sample testing on our own proprietary alloys before purchasing?
Absolutely. You can send material samples directly to our application laboratory. Our engineers will perform marking tests across various wavelengths (MOPA Fiber, UV, CO2), measure mark contrast and depth, and return a full optical analysis report along with marked samples free of charge.
What lead times and warranty terms apply to deliveries in Sweden?
Standard laser systems are delivered within 2 to 4 weeks depending on customer enclosure customization. Systems supplied through our authorized European distributor network include a comprehensive 3 to 5 year industrial warranty backed by factory technical engineers.
How do your laser systems integrate with automated factory networks in Linköping or Gothenburg?
Our control systems feature built-in digital I/O, Ethernet/IP, and RS232 interfaces, allowing direct communication with PLC networks, SCADA, Cobot arms, and Automated Data Matrix code verification cameras for 100% inline quality checking.
Upgrade Your Aerospace Part Identification Capabilities Today
Speak with our senior application engineers to review your engineering drawings, request material sample testing, or receive a customized technical quote for your Swedish manufacturing facility.